Key Takeaways:
- Match method to material: Ferromagnetic parts favor MPI; non-magnetic alloys and complex geometries suit FPI or eddy current.
- Defect location drives choice: Surface cracks call for FPI or MPI; subsurface and coated defects call for eddy current.
- Single-source accountability matters: Consolidating services under a qualified partner can simplify coordination and support consistent controls.
Choosing the wrong NDT method not only wastes time, but it can leave a defect undetected until the component is in service, where the consequences are far more severe than a failed inspection. FPI, MPI, eddy current, and borescope inspection each catch different flaws in different materials, and applying the wrong one is like using a metal detector to find a crack in glass; the tool simply is not built for the job.
At Valence, we’ve built one of the most comprehensive NDT platforms in aerospace surface finishing, supporting programs across commercial, defense, and space applications with audit-ready processes and NADCAP-accredited inspection capabilities.
In this piece, we will cover how FPI, MPI, eddy current, and borescope inspection compare, and how to choose the right method for your program.
What Is NDT Aerospace Inspection And Why Does Method Selection Matter?
NDT aerospace inspection detects flaws, cracks, porosity, inclusions, and corrosion in components without compromising their usability, and the method you specify directly determines which defects you’ll catch and which you’ll miss.
Method selection matters because no single technique covers every material, geometry, or defect type. Penetrant testing requires surface-connected discontinuities; MPI requires ferromagnetic material; eddy current requires electrical conductivity and has depth limitations. Selection also depends on the required flaw size, surface condition, accessibility, and the applicable procedure. For flight-critical parts, that decision carries safety, compliance, and schedule consequences.
Fluorescent Penetrant Inspection (FPI): How It Works And When To Use It
FPI is widely used to detect surface-connected discontinuities in compatible, nonporous metallic and nonmetallic components, regardless of magnetic properties.
How FPI works
A fluorescent dye is applied to a cleaned part and drawn into surface-breaking defects by capillary action. Excess penetrant is removed, developer is applied, and inspectors examine fluorescent indications under controlled UV-A and ambient-light conditions, evaluating them against acceptance criteria.
When to use FPI
Consider FPI for accessible, surface-connected discontinuities, such as open cracks, porosity, and laps, in compatible nonporous materials, including aluminum, titanium, and austenitic stainless steels, or on complex geometries where MPI magnetization is impractical. Select it against the specified inspection requirements, not magnetic properties alone.
Magnetic Particle Inspection (MPI): Strengths And Limitations
MPI detects surface and slightly subsurface discontinuities in ferromagnetic materials, including many steels, by magnetizing the part and applying magnetic particles that gather at flux leakage points.
Strengths
MPI is fast and sensitive to fine surface and near-surface cracks. It may detect discontinuities in certain thin coatings when the applicable specification permits and adequate sensitivity has been demonstrated. It is well-suited to high-volume inspection of ferrous forgings, castings, and machined steel parts.
Limitations
MPI works only on ferromagnetic materials, so it’s unsuitable for aluminum, titanium, or austenitic stainless steel. Sensitivity depends on magnetization direction and the inspection procedure, and demagnetization may be required.
Eddy Current Testing: How It Detects Subsurface Defects
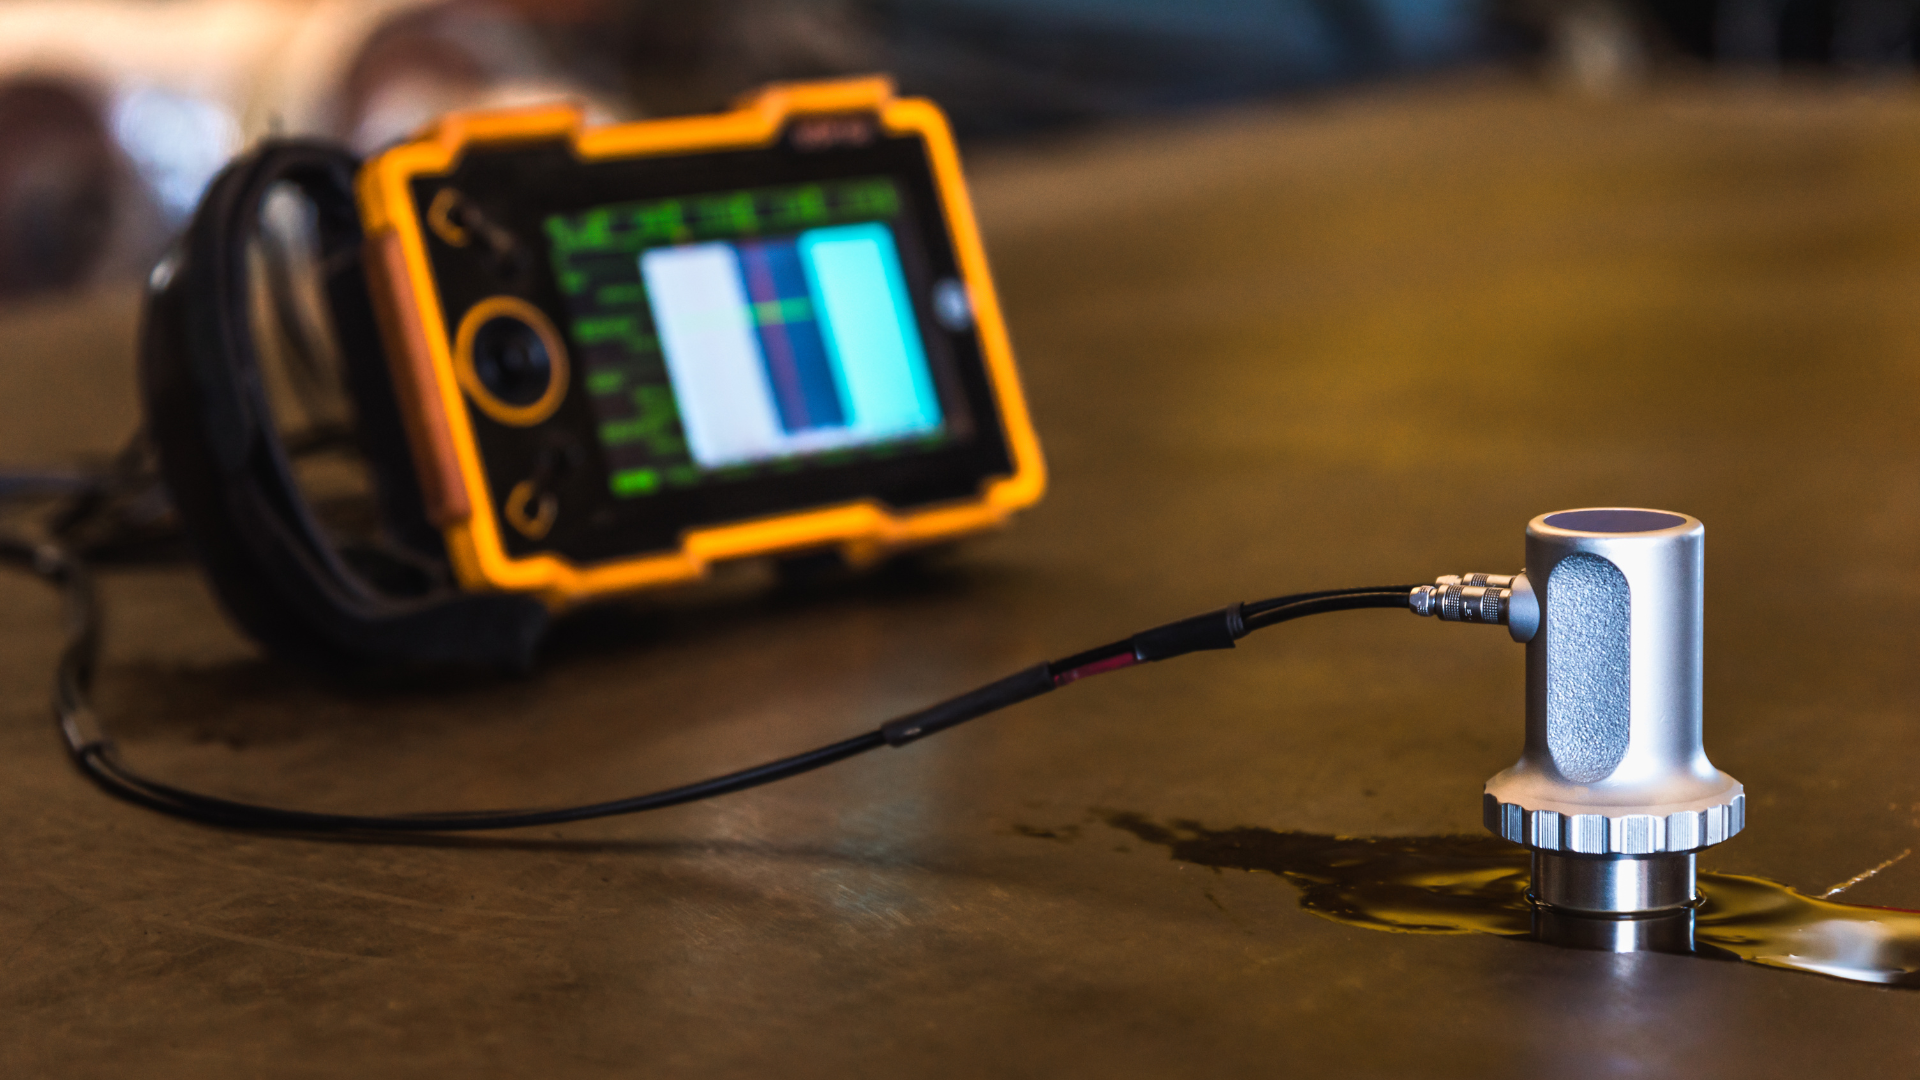
Eddy current uses electromagnetic induction to inspect conductive materials, often through suitable coatings and without penetrant chemicals or acoustic couplant.
How eddy current works
An alternating current in a probe coil induces circulating eddy currents in the part. Cracks, corrosion, or material changes disrupt those currents, and the probe registers the impedance shift. Because impedance changes can also reflect geometry, material properties, or probe spacing, interpretation requires proper calibration.
When to use eddy current
Eddy current is effective for surface cracks and selected near-surface or deeper applications when the probe, frequency, material, and calibration support the required detection. Penetration depends on frequency, conductivity, and permeability, with current density decreasing with depth.
Use it for corrosion under coatings, conductivity measurement, and, where validated correlations exist, assessment of heat-treatment or hardness-related material condition, and fastener-hole inspection in conductive metals. Suitable coatings may remain in place.
Borescope Inspection: Visual Access For Hard-to-Reach Components
Borescope inspection delivers magnified visual examination of internal or otherwise inaccessible areas, turbine cavities, engine passages, and closed assemblies, using a flexible or rigid optical probe.
How borescope inspection works
Optical or video borescopes provide illuminated views of otherwise difficult-to-access surfaces through a suitable access opening, allowing inspectors to assess internal surfaces for cracks, wear, foreign-object damage, and corrosion. Detection depends on visibility, resolution, lighting, and surface condition.
When to use borescope
Choose borescope inspection when the area of interest can’t be reached or disassembled economically, or for in-service engine and assembly checks. It’s a visual method, so it detects what’s visible within the line of sight, not subsurface flaws.
Comparing NDT Methods: Which One Fits Your Component And Defect Type
The right method depends on three variables: material, defect location, and geometry.
Match by material and defect
- Non-magnetic alloys, surface cracks: FPI
- Ferromagnetic steels, surface/near-surface cracks: MPI
- Conductive metals, surface or near-surface defects: Eddy current
- Internal/inaccessible visual inspection: Borescope.
Sensitivity and trade-offs
MPI, FPI, and eddy current can each provide high sensitivity to surface cracks in suitable applications; select the procedure that demonstrates the required detection capability for the component and flaw. Among these methods, MPI and eddy current can detect some subsurface discontinuities within application-specific limits, while FPI requires a surface connection and borescopes inspect visible surfaces.
How Valence Selects And Applies The Right NDT Method For Aerospace Programs
We select NDT methods by starting with your part, its alloy, geometry, criticality, and the specific defects that threaten it, then matching the technique to the requirement and the applicable specification.
Our process
We review drawing callouts, customer specifications, and industry standards, then select and apply inspection procedures to meet specified detection requirements, using applicable qualification evidence and capability demonstrations where required. Where a single method leaves a gap, we build a multi-method inspection plan.
The Valence Standard
Valence’s common QMS is intended to support consistent controls across its network; site-specific capabilities and approvals should be verified. To learn more about the full range of capabilities we bring to every program, explore our Valence Services Overview.
Final Thoughts
Choosing the right NDT aerospace method isn’t about picking a favorite; it’s about matching physics to your part, defect, and specification. FPI and MPI detect surface cracks; eddy current detects surface and near-surface flaws; and borescope reveals the unreachable. Get the match wrong, and you risk missed defects or wasted rejections. Partner with a qualified provider who selects methodically, and inspection becomes a source of program confidence rather than risk.
Frequently Asked Questions About Choosing The Right NDT Method: FPI vs. MPI vs. Eddy Current vs. Borescope
Which nondestructive testing method should I specify for my aerospace program?
Specify based on material and defect type: FPI for non-magnetic surface cracks, MPI for ferrous surface cracks, eddy current for surface or subsurface defects in conductive metals, and borescope for internal visual access. Complex programs often need more than one method.
How do I know if I need FPI or eddy current testing?
Choose FPI for surface-breaking cracks on compatible parts you can clean and access. Choose eddy current for conductive materials, including inspection through suitable coatings and in fastener holes, since it can detect certain flaws that FPI cannot reach.
What aerospace standards and certifications should my NDT method comply with?
Follow applicable drawings, maintenance instructions, customer requirements, and specified procedures. Verify required facility accreditation (e.g., Nadcap), QMS certification (e.g., AS9100), and personnel qualification separately, using contractually applicable revisions of ASTM E1417/E1417M and E1444/E1444M where specified.
Can I combine multiple NDT methods, and when is a multi-method strategy necessary?
Yes, combining methods is common for flight-critical parts. A multi-method strategy is necessary when one technique can’t cover all defect types or locations, such as pairing FPI for surface cracks with eddy current for subsurface flaws.
Which NDT method is best for crack detection in welds?
MPI is commonly used for surface and slightly subsurface cracks in ferromagnetic welds; FPI is suitable for surface-connected discontinuities in compatible, nonporous weld materials such as aluminum or titanium. Embedded-flaw inspection requires another suitable technique.
Which NDT method is most sensitive to surface cracks?
MPI, FPI, and eddy current can each provide high sensitivity to surface cracks in suitable applications. Select the procedure that demonstrates the required detection capability rather than relying on the method name alone.