Key Takeaways:
- Thickness Decides The Method: Method A uses an X-cut for coatings thicker than 5 mils, while Method B uses a cross-cut lattice for coatings up to 5 mils.
- Two Rating Scales: Method A results run from 5A to 0A, and Method B results run from 5B, with no removal, to 0B, with more than 65 percent of the area removed.
- Pass/Fail Comes From The Spec: ASTM D3359 defines how to test and rate adhesion, while the coating or OEM specification sets the minimum acceptable rating.
A coating can meet every thickness and appearance requirement and still lift from the substrate in service. ASTM D3359 is one of the most widely referenced ways to check that a finish is bonded before it ships.
Valence Surface Technologies, the world’s largest independent aerospace surface finishing company, applies primers, topcoats, and specialty coatings for more than 3,000 global customers under one common quality management system.
This guide explains how Methods A and B work, how results are rated, and how aerospace programs apply them.
The Purpose Of ASTM D3359 In Coating Quality Control
ASTM D3359 gives a fast, qualitative way to judge whether a coating is bonded to its substrate by cutting through the film, applying pressure-sensitive tape, and rating how much coating the tape removes. The current edition, D3359-23, contains two methods selected primarily by film thickness. The tests are suited to quality control and process verification, but they do not measure bond strength quantitatively, which is the role of pull-off methods such as ASTM D4541.
Valence applies aerospace paint systems as part of an integrated offering that also includes NDT, chemical processing, specialty plating, shot peening, and sub-assembly. Explore our Valence Services Overview for the full range of coating capabilities.
ASTM D3359 Method A: The X-Cut Tape Test
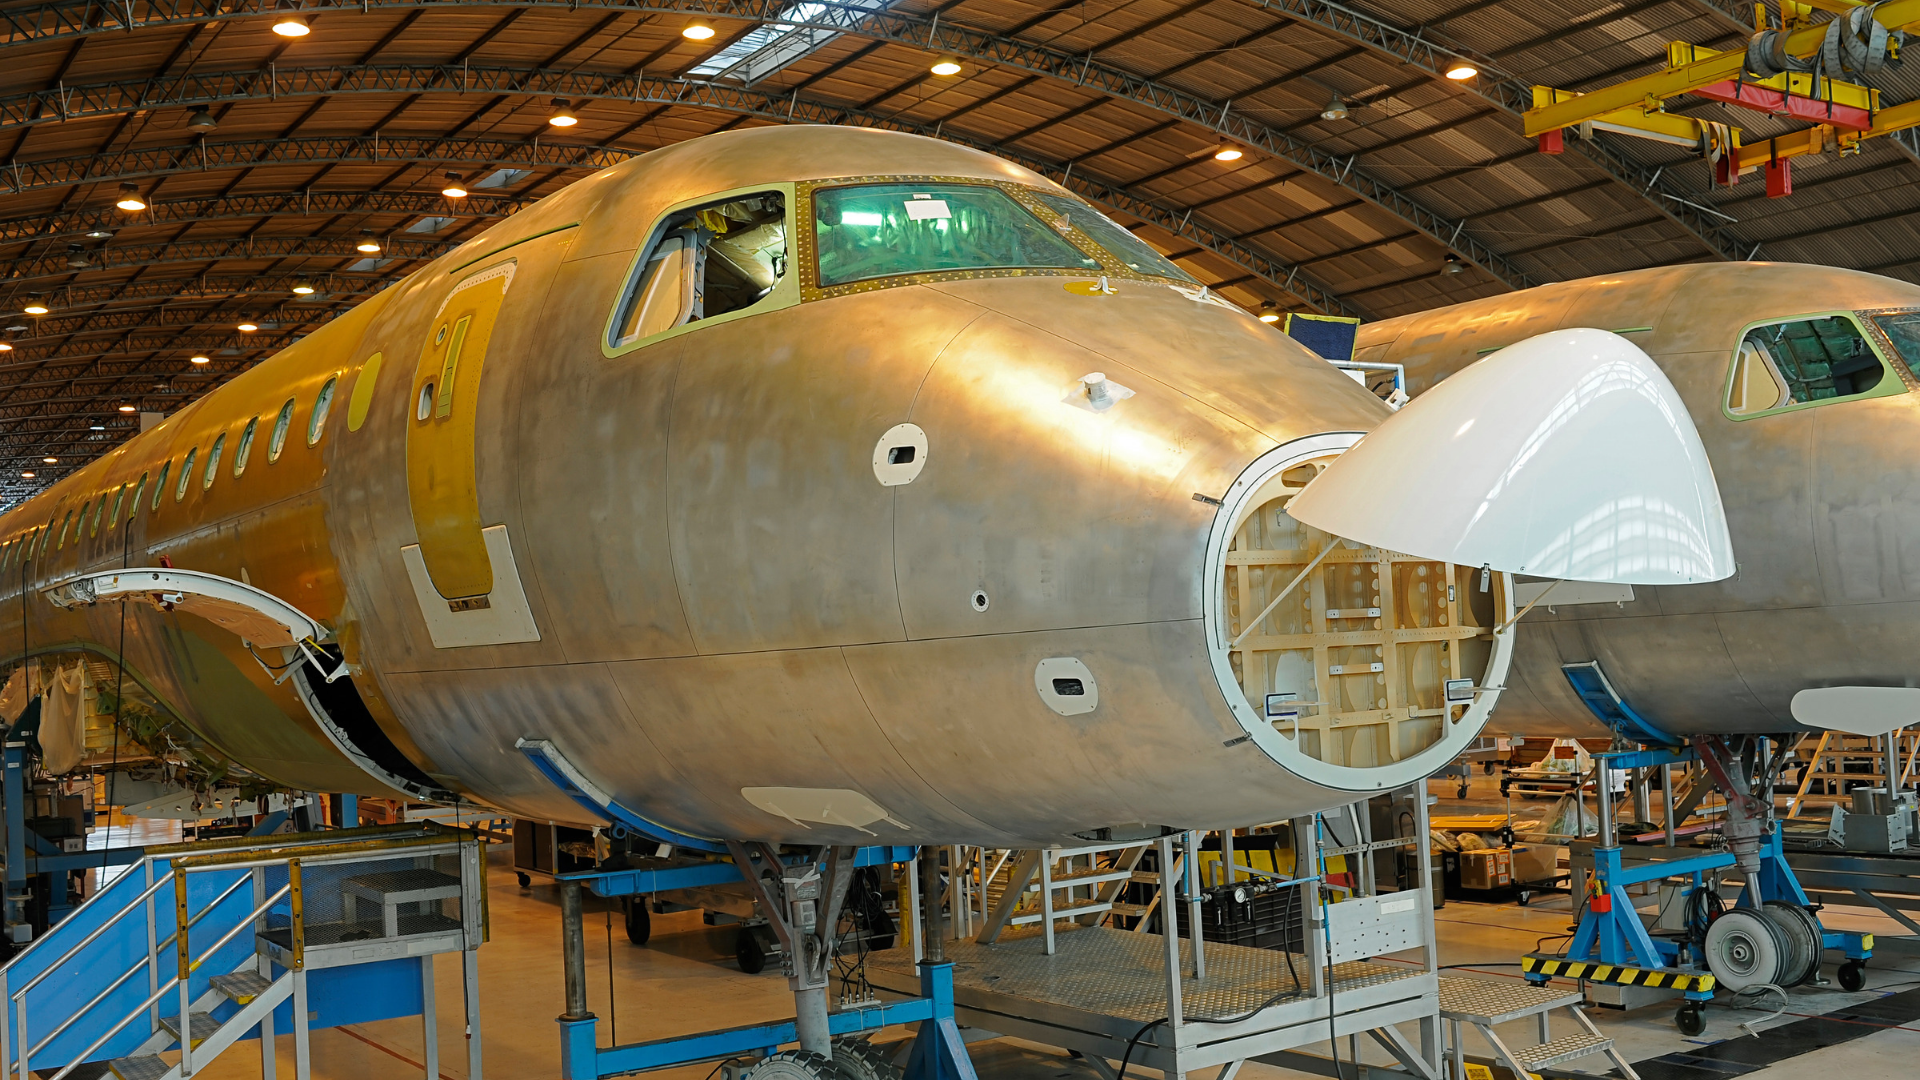
Method A evaluates adhesion with a single X-shaped incision and is the simpler of the two procedures.
When Method A Applies
Method A is intended for coatings thicker than 5 mils, or 125 µm, and is primarily used in the field. Its single cut makes it practical on large structures, though the results are more subjective than a lattice test.
Making The X-Cut And Applying Tape
The technician makes two cuts about 1.5 inches long through the film to the substrate, intersecting near their midpoints at an angle of 30 to 45 degrees. Tape is pressed firmly over the intersection and removed within 90 ± 30 seconds by pulling it rapidly back on itself at an angle as close to 180 degrees as possible.
Reading The 5A To 0A Scale
A 5A rating means no peeling or removal, and 4A indicates trace peeling along the incisions or at their intersection. Ratings of 3A and 2A reflect jagged removal extending up to 1/16 inch and 1/8 inch from the cuts, while 1A and 0A indicate removal across most of the X or beyond it.
ASTM D3359 Method B: The Cross-Cut Tape Test
Method B uses a lattice of cuts to rate adhesion across a defined grid, giving more repeatable results on thinner films.
When Method B Applies
Method B covers coatings up to 5 mils, or 125 µm, and is best suited to laboratory and shop settings. That range includes most aerospace primer and topcoat systems.
Cut Spacing Based On Coating Thickness
Films up to 2 mils receive 11 parallel cuts spaced 1 mm apart, while films from 2 to 5 mils receive 6 cuts spaced 2 mm apart. A second set of cuts at 90 degrees forms the lattice, and every cut must reach the substrate for the test to be valid.
Interpreting 5B To 0B Results
What do ASTM D3359 ratings 5B to 0B mean? Each rating corresponds to the share of the lattice area removed by the tape:
- 5B: edges are smooth, and no squares are detached
- 4B: small flakes detach at intersections, affecting less than 5 percent of the area
- 3B: small flakes detach along edges and intersections, affecting 5 to 15 percent
- 2B: coating flakes along edges and parts of squares, affecting 15 to 35 percent
- 1B: large ribbons and whole squares detach, affecting 35 to 65 percent
- 0B: flaking and detachment exceed 65 percent of the area
Applying ASTM D3359 To Aerospace Paint Systems
How do you test paint adhesion on aerospace parts? Most programs use ASTM D3359 or an OEM tape test method, run on production parts, on test panels processed alongside them, or both. Many coating specifications include a wet-tape adhesion step, in which the painted panel is immersed in water before testing, because moisture exposure reveals weak pretreatment or primer bonds that a dry test may miss. Some OEMs maintain their own procedures, such as Boeing’s BSS 7225, so the governing drawing or process specification determines which method applies and the minimum acceptable rating.
Adhesion failures usually trace back to steps that happen before paint, including inadequate cleaning, an incorrect conversion coating or anodize, contamination, or a missed recoat window. At Valence, painting is integrated with the chemical processing that precedes it, so pretreatment, primer, topcoat, and adhesion testing are managed in one routing under the Valence Standard. That continuity gives quality teams a single record to review when an adhesion result needs to be traced to its cause.
Final Thoughts
Adhesion is the foundation that every other coating requirement depends on once a part enters service. A tape test rating carries real value only when it reflects disciplined surface preparation, controlled application, and testing to the correct specification. Valence manages pretreatment, painting, and adhesion verification under one quality system across twelve facilities, helping aerospace, defense, and space manufacturers deliver finishes that perform as specified.
Frequently Asked Questions About ASTM D3359 Tape Adhesion Testing
How is ASTM D3359 different from ISO 2409?
ISO 2409 is a similar cross-cut test, but its 0 to 5 classification treats 0 as the best adhesion, the reverse of the ASTM D3359 B scale.
What tools are needed to perform an ASTM D3359 test?
A typical kit includes a sharp blade or multi-blade cutter, a cutting guide, pressure-sensitive tape, a soft brush, a pencil eraser for pressing the tape, and an illuminated magnifier.
Why does blade condition matter in adhesion testing?
A dull blade can tear or chip the coating along the cuts, lowering the rating even when the coating is well bonded.
Can ASTM D3359 be performed on curved surfaces?
Flat areas give the most reliable results, since curvature makes it harder to cut evenly and keep the tape in full contact.
Do temperature and humidity affect tape test results?
Yes, ambient conditions can change how the tape and coating behave, so specifications often call for testing under controlled conditions.
Is ASTM D3359 a destructive test?
Yes, the cuts damage the coating, so testing is usually performed on test panels or noncritical areas unless the specification permits repair.